Refined Palm Oil (specifically RBD Palm Olein) is the liquid fraction obtained from the fractionation of crude palm oil (CPO) harvested from the mesocarp of oil palm fruits (Elaeis guineensis). Through precise multi-stage physical refining, the oil is neutralized, clarified, and deodorized to eliminate free fatty acids, moisture, and impurities while preserving natural beta-carotenes and tocopherols.
It remains naturally semi-solid at lower temperatures and crystal-clear liquid at standard ambient temperatures (Cloud Point: 8°C - 10°C). Free from chemical hydrogenation and cholesterol, it is internationally recognized as the most versatile, cost-effective, and shelf-stable vegetable cooking oil in the global food processing industry.
Our manufacturing process utilizes state-of-the-art European automated continuous physical refining technology:
1. Harvesting & Sterilization: Fresh Fruit Bunches (FFB) from certified sustainable RSPO plantations are steam-sterilized within 24 hours of harvest to arrest enzymatic breakdown.
2. Mechanical Pressing & Clarification: Pure crude palm oil is extracted via twin-screw mechanical expellers without harsh synthetic solvents.
3. Pre-treatment & Degumming: Phosphatides and trace gums are removed using food-grade natural phosphoric acid under strict temperature monitoring.
4. Bleaching: Adsorption using natural activated bleaching earth removes residual trace pigments, heavy metals, and oxidation precursors.
5. Deodorization & Deacidification: High-vacuum steam distillation at 240°C–260°C strips volatile odor compounds and reduces Free Fatty Acids (FFA) to below 0.08%.
6. Dry Fractionation: Controlled crystallization and high-pressure membrane filtering separate the crystal stearin from the crystal-clear liquid olein fraction (CP8 / CP10).
7. Nitrogen Blanketing & Loading: Stored under food-grade inert nitrogen in stainless-steel storage silos prior to flexitank and containerized bottling at Penang Port.
• 100% Naturally Trans-Fat Free: Unlike partially hydrogenated alternative shortenings, palm oil delivers natural structural solidity without generating dangerous trans fatty acids.
• Rich in Natural Vitamin E: Packed with potent tocotrienols and alpha-tocopherols that act as powerful cellular antioxidants and extend food shelf-life naturally.
• Balanced Fatty Acid Profile: Composed of approximately 50% saturated and 50% unsaturated (oleic and linoleic) fatty acids, providing superior heart stability compared to animal fats.
• Zero Cholesterol & Sodium: Naturally vegetable-derived and heart-healthy when consumed as part of a balanced diet.
• High Caloric Density & Bioavailability: Provides a highly digestible, clean energy source essential for nutritional food fortification and dairy fat replacement.
Laboratory tested in accordance with AOCS and CODEX Alimentarius international standards.
| Parameter / Test Method | Specification Limit / Guaranteed Value |
|---|---|
| Free Fatty Acid (% as Palmitic) | Max 0.08% |
| Moisture & Impurities (M&I) | Max 0.08% |
| Iodine Value (Wijs) | Min 56.0 – 60.0 g I2/100g |
| Slip Melting Point | Max 24.0°C |
| Cloud Point | Max 8.0°C (CP8 Grade) |
| Color (Lovibond 5¼" Cell) | Max 2.5 Red / 25.0 Yellow |
| Peroxide Value | Max 1.0 meq O2 / kg |
| Smoke Point | Min 235°C (455°F) |
| Refractive Index (40°C) | 1.4580 – 1.4600 |
| Saponification Value | 190 – 205 mg KOH/g |
| Unsaponifiable Matter | Max 1.0% |
| Heavy Metals (Lead / Arsenic) | Max 0.1 mg/kg / Max 0.1 mg/kg |
| Cholesterol | Nil / 0.0 mg |
| Purity & Appearance | Clear golden liquid, free from rancidity and foreign matter |
• Industrial Deep Frying: The premier oil for commercial potato chips, instant ramen noodles, extruded snacks, donuts, and quick-service restaurant frying due to its ultra-high smoke point (235°C) and resistance to polymer breakdown.
• Bakery & Confectionery: Acts as a premium shortenings base, dough conditioner, and creaming medium for biscuits, cookies, pastries, and chocolate compound fillings.
• Dairy Fat Alternatives & Margarine: Essential base fat for condensed milk formulations, non-dairy coffee creamers, whipped toppings, and table margarines.
• Canned Food & Sauce Emulsions: Used in canned fish packing, chili paste preservation, bouillon cubes, and savory ready-meal gravies.
• Oleochemical & Personal Care: Serves as a raw ingredient for pharmaceutical excipients, natural soaps, and cosmetic grade glycerins.
Spot Price: $890 USD / MT (CIF). Submit your tonnage and destination port for an expedited quotation.
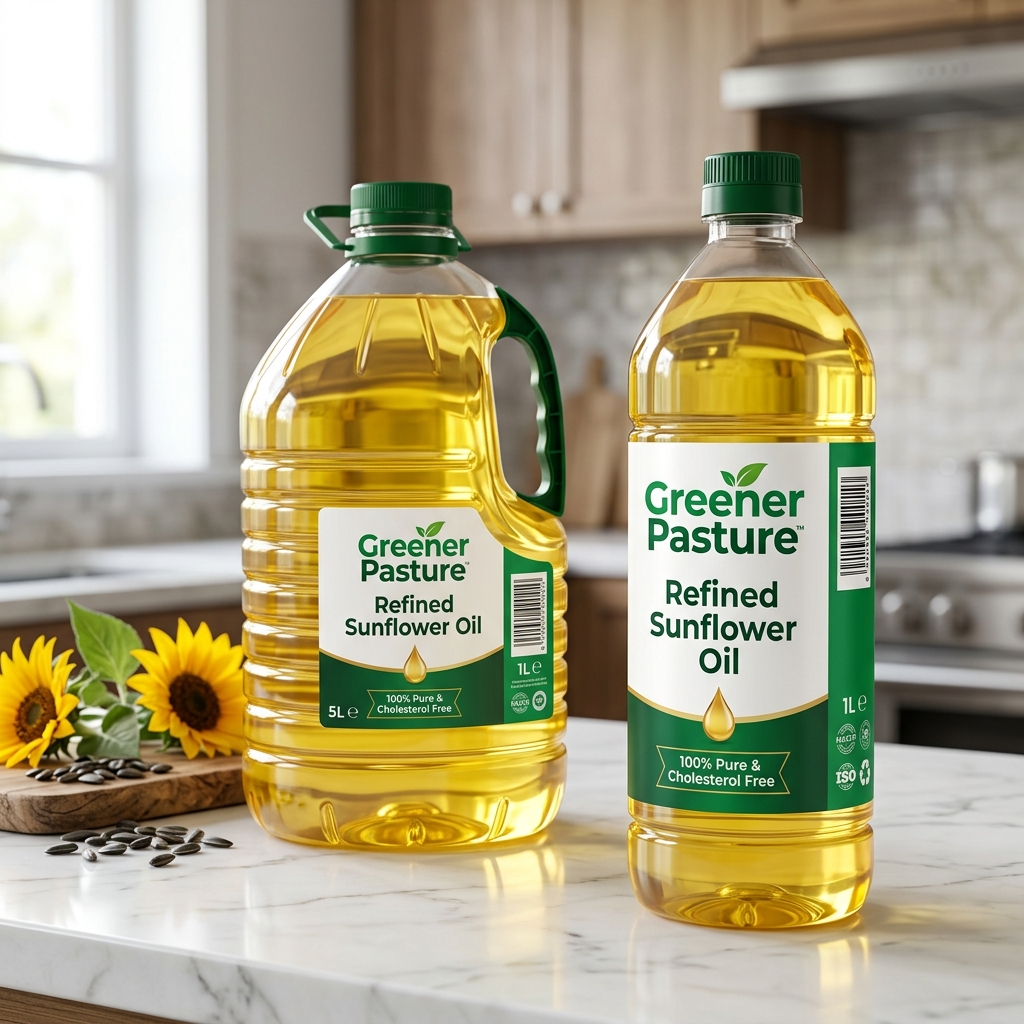
Premium light-golden cooking oil extracted from selected sunflower seeds (Helianthus annuus), fully refined, bleached, and deodorized. Renowned for its delicate neutral taste, light viscosity, and rich natural Vitamin E content.
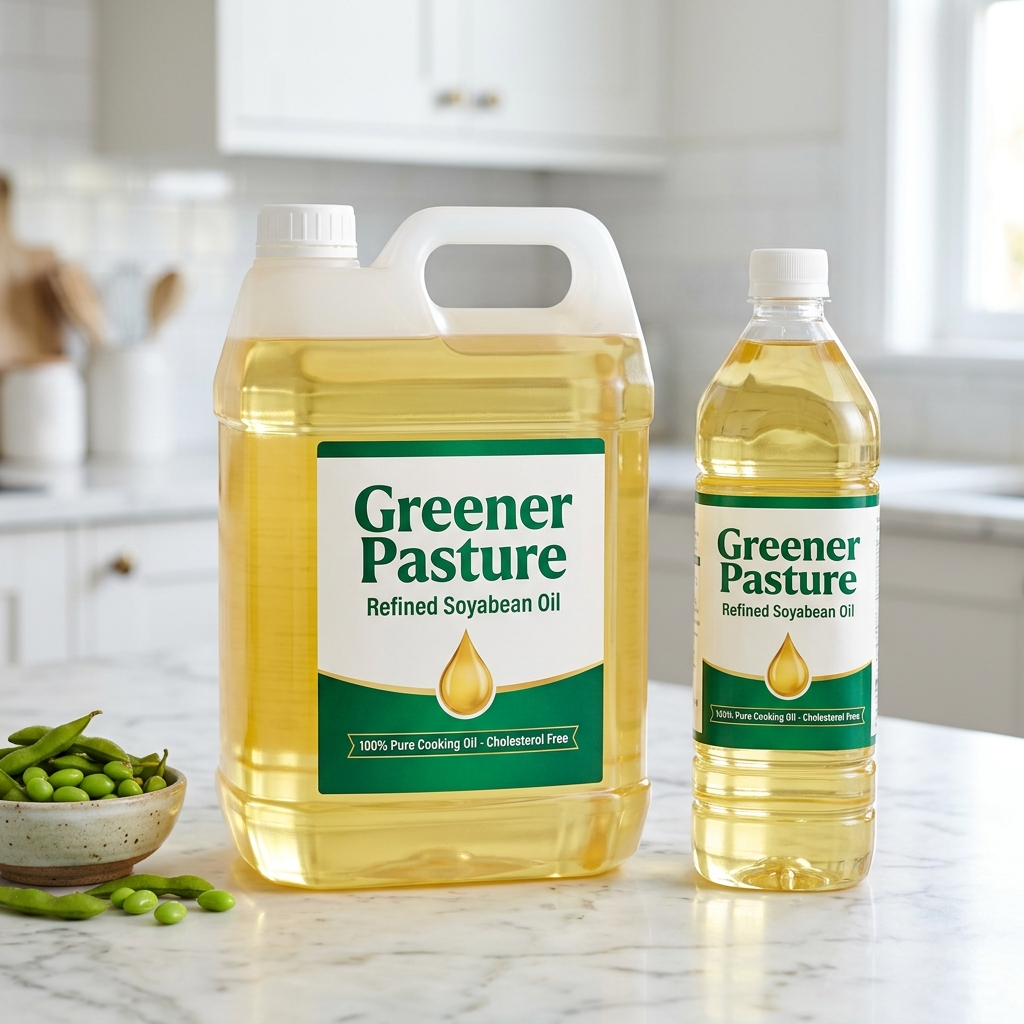
High-grade 100% pure refined soybean oil pressed from premium non-GMO soybeans. Features a balanced fatty acid profile, high thermal stability, and essential polyunsaturated lipids for food manufacturing and culinary applications.
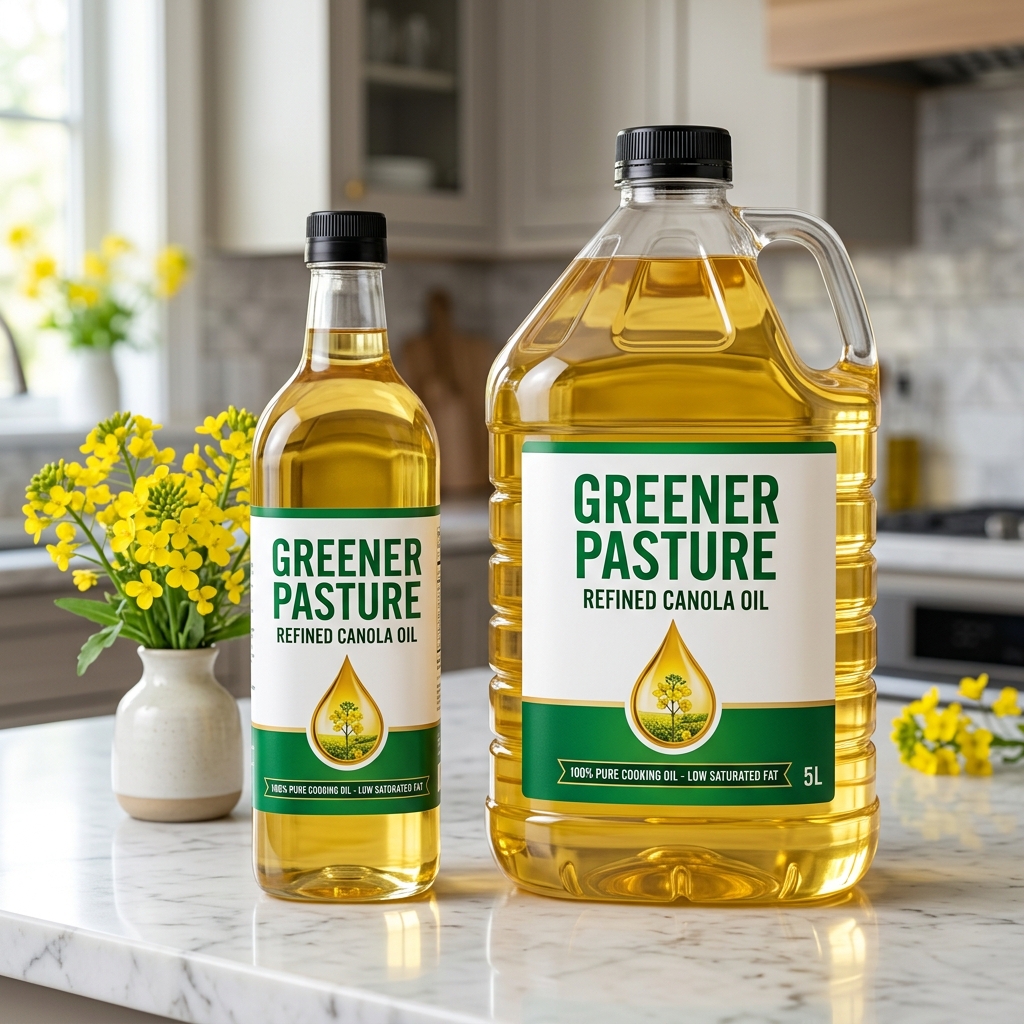
Certified low-erucic-acid rapeseed oil refined to peak purity. Boasting one of the lowest saturated fat contents of any edible oil (under 7%) and an optimal Omega-6 to Omega-3 ratio (2:1).